Project context
This page addresses manufacturing quality management for OEM quality leaders, engineers and sourcing teams who need confidence that component, tooling and final-assembly decisions will be reviewed in a controlled way. It is designed to make the buyer's next manufacturing decision clearer by linking the product requirement, process route and approval evidence before cost, tooling or schedule commitments become difficult to change.
What qualification needs to solve
Quality Management for Multi-Process Industrial Product Programs is relevant when a buyer needs to turn critical drawings and specifications, product-risk notes, approved samples, inspection expectations, component acceptance criteria, functional-test requirements, packaging needs and the customer escalation path into a credible route. Start by confirming the product function, end use, interfaces, expected quantity and decision owner. That separates information that can be resolved through engineering review from questions that need a prototype, tool trial, supplier check or controlled sample.
How the project route should be evaluated
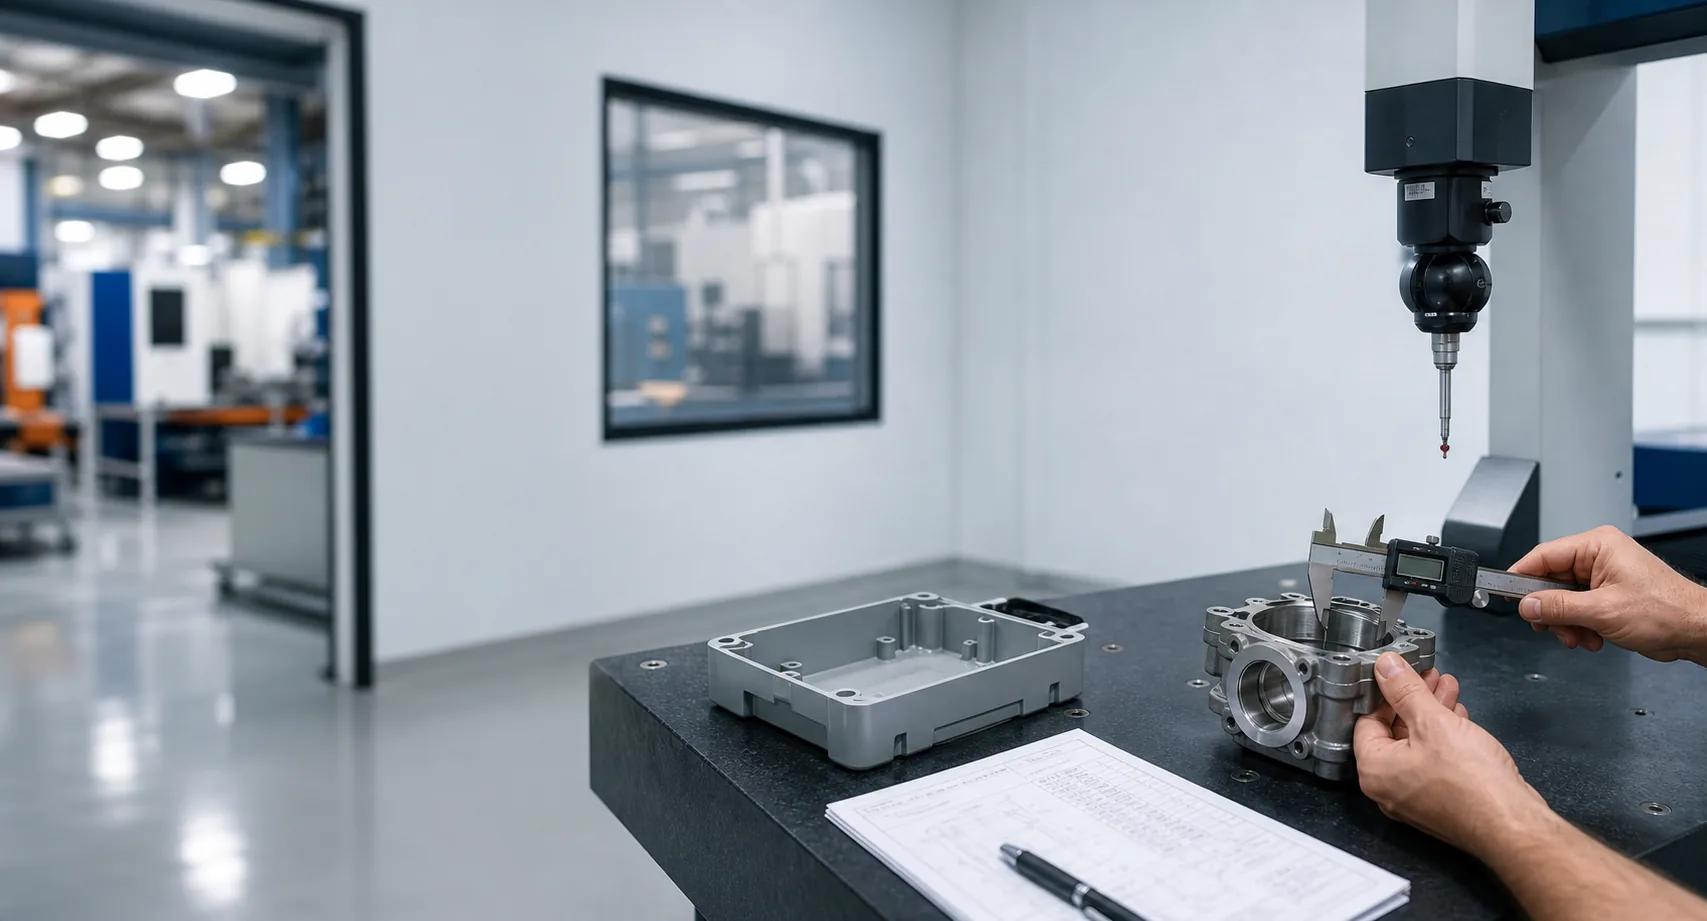
The work in scope is quality planning, sample and change-control gates, incoming-component checks, in-process controls, assembled-product verification, nonconformance communication and documentation handover. Engineering review should expose the interfaces that can create avoidable risk: where one part supports another, where a seal or fastener affects access, where a cable, port or purchased component needs clearance, and where a material or feature changes the selected process. A practical DFM or feasibility recommendation states what should change, why it matters and which product requirement it protects.
Where evidence and responsibility need to be visible
quality planning begins with the product requirement, then follows the project through prototype, tooling trials, production, assembly and delivery rather than appearing only at final shipment is the operational backbone. Process choice should follow geometry, expected volume, material behavior, finish, assembly sequence, service access and the evidence needed for release. A parting line, port position, bend relationship, fastening strategy, coating choice or material specification is part of the product architecture, not a late manufacturing detail.
critical-to-function features, approved evidence, inspection responsibilities, traceable change decisions and rapid escalation when a result does not match the agreed requirement When a program uses purchased items or final assembly, responsibility should be visible before parts arrive: supplied components need an approval basis, interfaces need a fit plan and the final build needs a check that reflects use. Material selection should be confirmed against the actual operating environment, load, appearance, process route and buyer-required documentation rather than treated as a generic online option. Accessory matching should include the parts that create real interface risk: inserts, seals, fasteners, cable hardware, labels, purchased modules, packaging and the fixtures or instructions needed to assemble them. Those controls reduce the chance that an assembly station becomes the first place a mismatch is discovered.
Commercial, quality and delivery controls
MOQ is a project variable, not a generic marketing number. It follows the process route, tooling or setup investment, component sourcing, material, finish and forecast. Freeze custom requirements through released drawings, material specifications, component interfaces and approved samples. Color, texture, coating, marking, print, labels and cosmetic acceptance should be defined with an approved reference whenever they affect the finished product. The buyer should define product, material, market and customer compliance requirements early. Pauline can coordinate the agreed manufacturing evidence, but no unverified certification or performance claim should be implied by a web page. Timing should be planned around the actual decision gates: design review, samples, tooling, components, approvals, production and final-build verification. MOQ depends on the process, tooling investment, part complexity, material and demand forecast, so it should be documented for the project rather than promised as a generic threshold. The purpose is to give the buyer a comparison basis that protects the product, schedule and accountability line.
Next step
Bring the product context. We will help define the manufacturing conversation.
Use the quick enquiry for a fast route discussion, or use the detailed project form to share CAD, drawings, a sample description or an existing tooling issue.
Request a Quote →