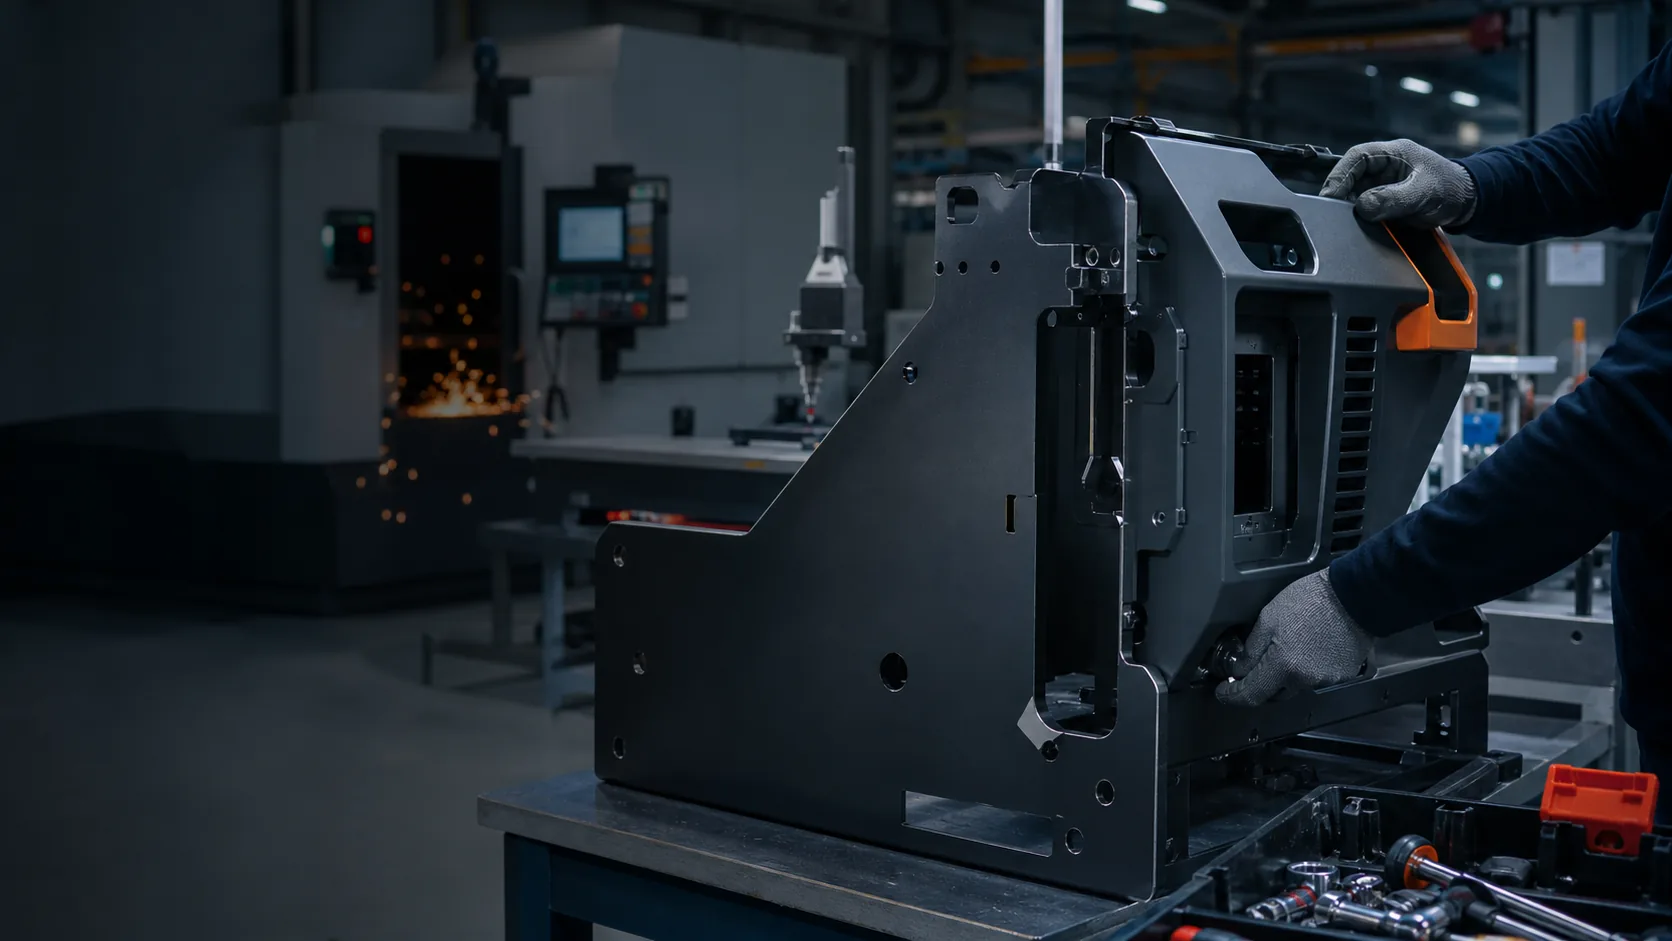
Large fabricated structure
Panel flatness, frame squareness and weld sequence affect door, seal and module fit.

Engineering Case Study
A case framework for controlling cabinets, brackets, thermal hardware, bought-out components and mechanical assembly without overstating electrical or certification scope.
01 / Project Brief
This brief makes the relationship between application, process, material, buyer input and evidence clear before the detailed engineering narrative.
02 / Project Background
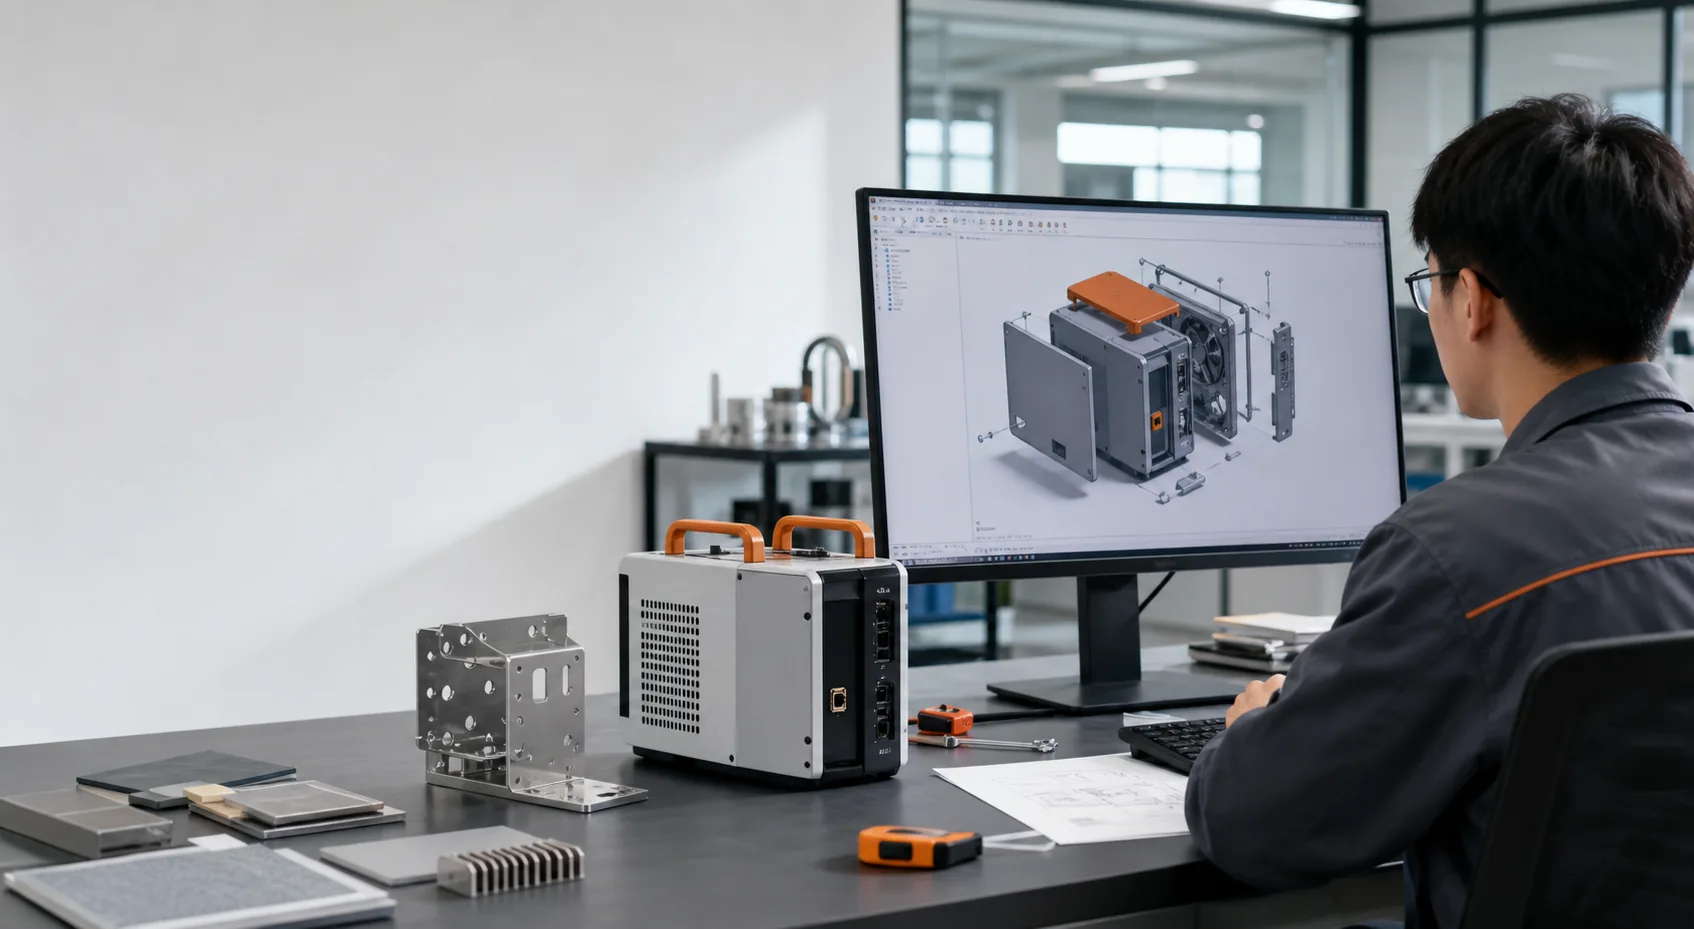
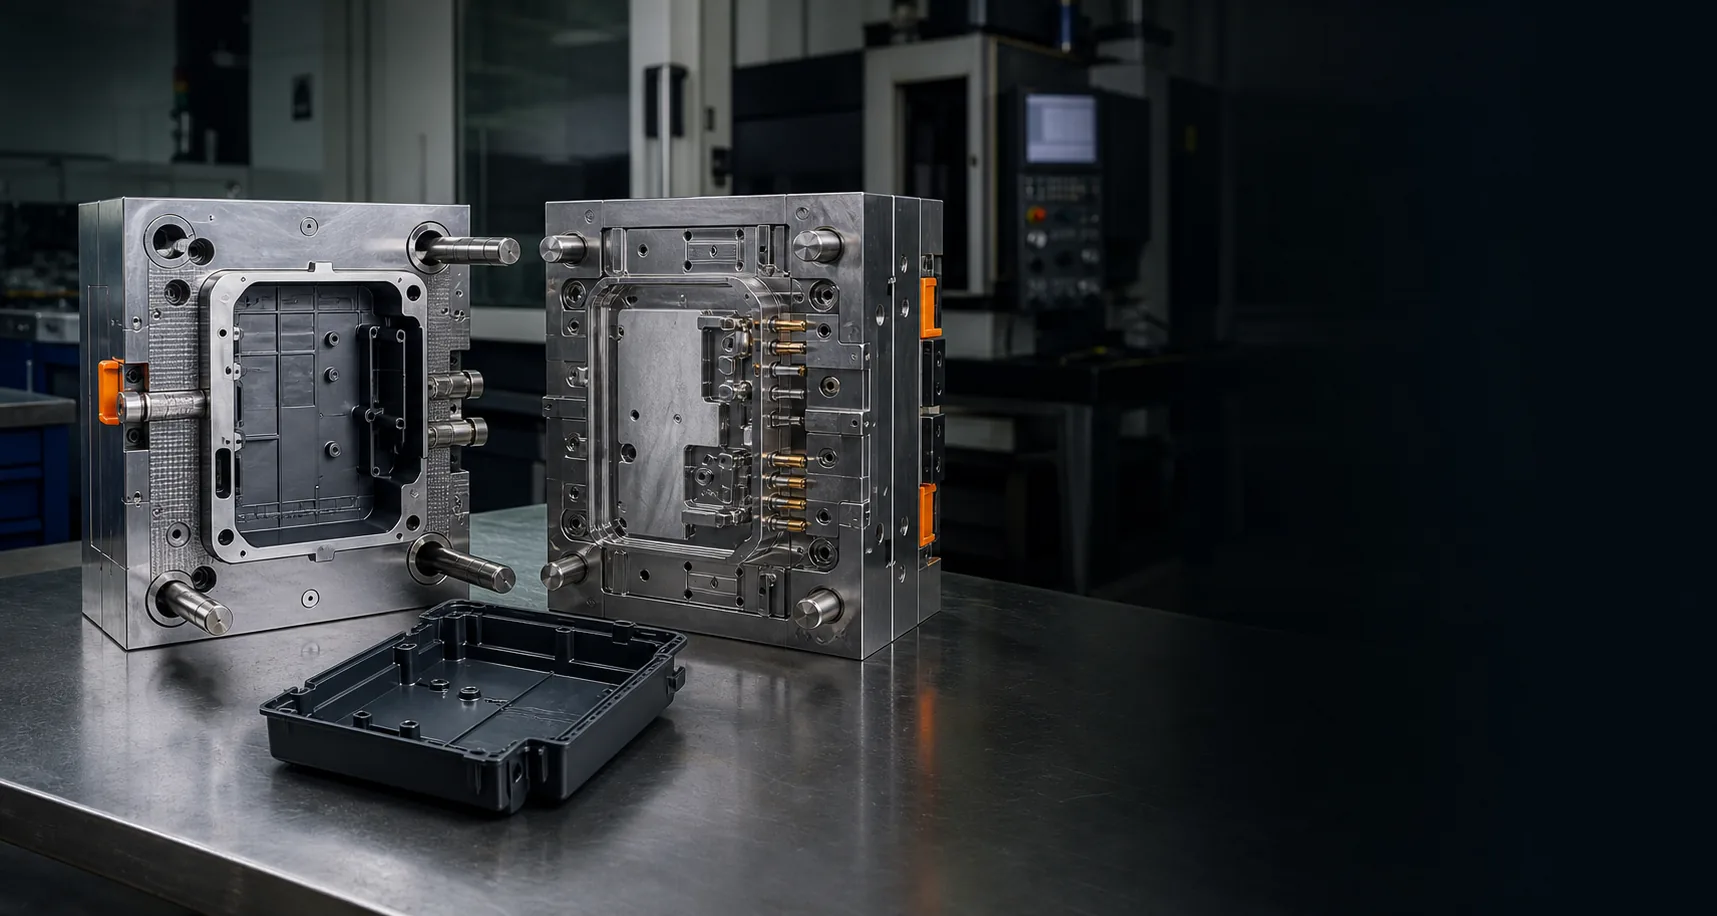
The program combines a fabricated cabinet, internal rails and brackets, molded or machined protection parts, thermal-management hardware, fasteners, seals and buyer-specified electrical modules.
A reliable quotation requires a responsibility matrix. The buyer must identify which components arrive as consigned parts, which are sourced by Pauline, which mechanical checks are required and which electrical or regulatory tests remain outside Pauline's scope.
The engineering route focuses on repeatable mechanical assembly, interface control, traceable changes and packing suitable for the destination and installation sequence.
03 / The Challenge
Panel flatness, frame squareness and weld sequence affect door, seal and module fit.
Rails, lifting points and assembly fixtures must protect operators and controlled interfaces.
Fans, ducts and heat-transfer components need defined clearances and fastening.
Purchased parts and customer-supplied modules must match the controlled BOM and revision.
Mechanical quality evidence must not be confused with electrical safety or system certification.
04 / Engineering Analysis and DFM
Every review item should identify the question, responsible owner and evidence needed before tooling, production or assembly moves forward.
| Review area | Engineering question | Release evidence |
|---|---|---|
| Cabinet structure | Review datums, weld sequence, flatness, doors, access and coating allowance. | Fabrication drawing and fixture plan |
| Internal hardware | Check rails, brackets, fastener access and module installation sequence. | Assembly model and work instruction |
| Bought-out parts | Confirm specification, approved source, incoming criteria and substitution control. | Approved vendor/BOM record |
| Handling | Define lifting, transport restraint and assembly aids for heavy components. | Handling plan and fixture check |
| Validation | Define mechanical, appearance and packing evidence; identify buyer-owned tests. | Responsibility matrix and release checklist |
05 / Selected Solution
Freeze cabinet and module datums, validate installation access with a pilot build, control purchased components through the approved BOM and document the mechanical inspection boundary. Assembly fixtures and work instructions are updated from actual build findings before production release.
The final route remains project-specific. Cost, MOQ and lead time become reliable only after materials, files, component responsibility, acceptance criteria and change ownership are confirmed.
Solution controls
06 / Manufacturing Route
Use, CAD, sample, components, volumes and open decisions.
Map architecture, interfaces, scope and evidence.
Test the highest-risk fit, access or functional assumptions.
Close process, tolerance, finish and assembly risks.
Release tools and fixtures against controlled files.
Produce parts through approved process plans.
Validate bought-out parts and complete-product interfaces.
Control changes, packing, records and delivery.
Review process fit, interfaces, evidence, MOQ, lead time and buyer inputs for this project stage.
Review related service →Review process fit, interfaces, evidence, MOQ, lead time and buyer inputs for this project stage.
Review related service →Review process fit, interfaces, evidence, MOQ, lead time and buyer inputs for this project stage.
Review related service →Review process fit, interfaces, evidence, MOQ, lead time and buyer inputs for this project stage.
Review related service →07 / Quality and Validation
A credible project record names the check, method, sample or record and approval owner. Generic quality claims do not replace project-specific acceptance criteria.
Frame squareness, panel flatness, hole position, door movement and coating
Part number, revision, incoming condition and approved substitution status
Torque, access, clearance, restraint and mechanical functional checks
Pilot record, approved sample, inspection plan, packing and change control
08 / Project Result
These release outcomes describe the intended evidence structure.
Review Pauline quality management →Evidence-led outcome framework
09 / Production Evidence
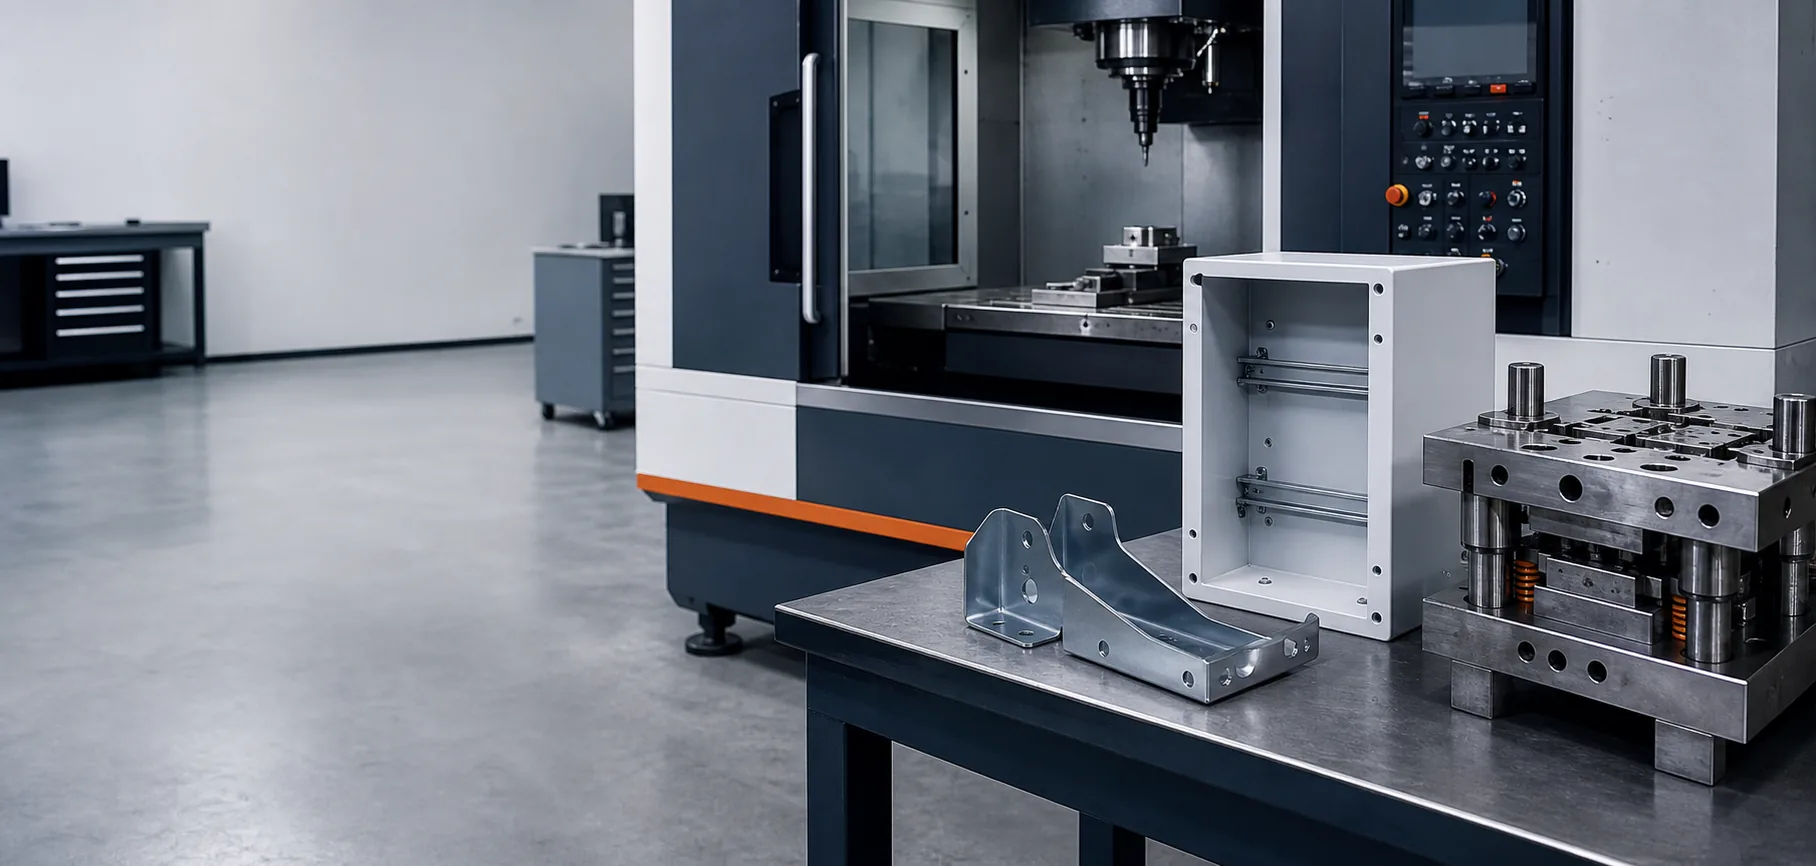
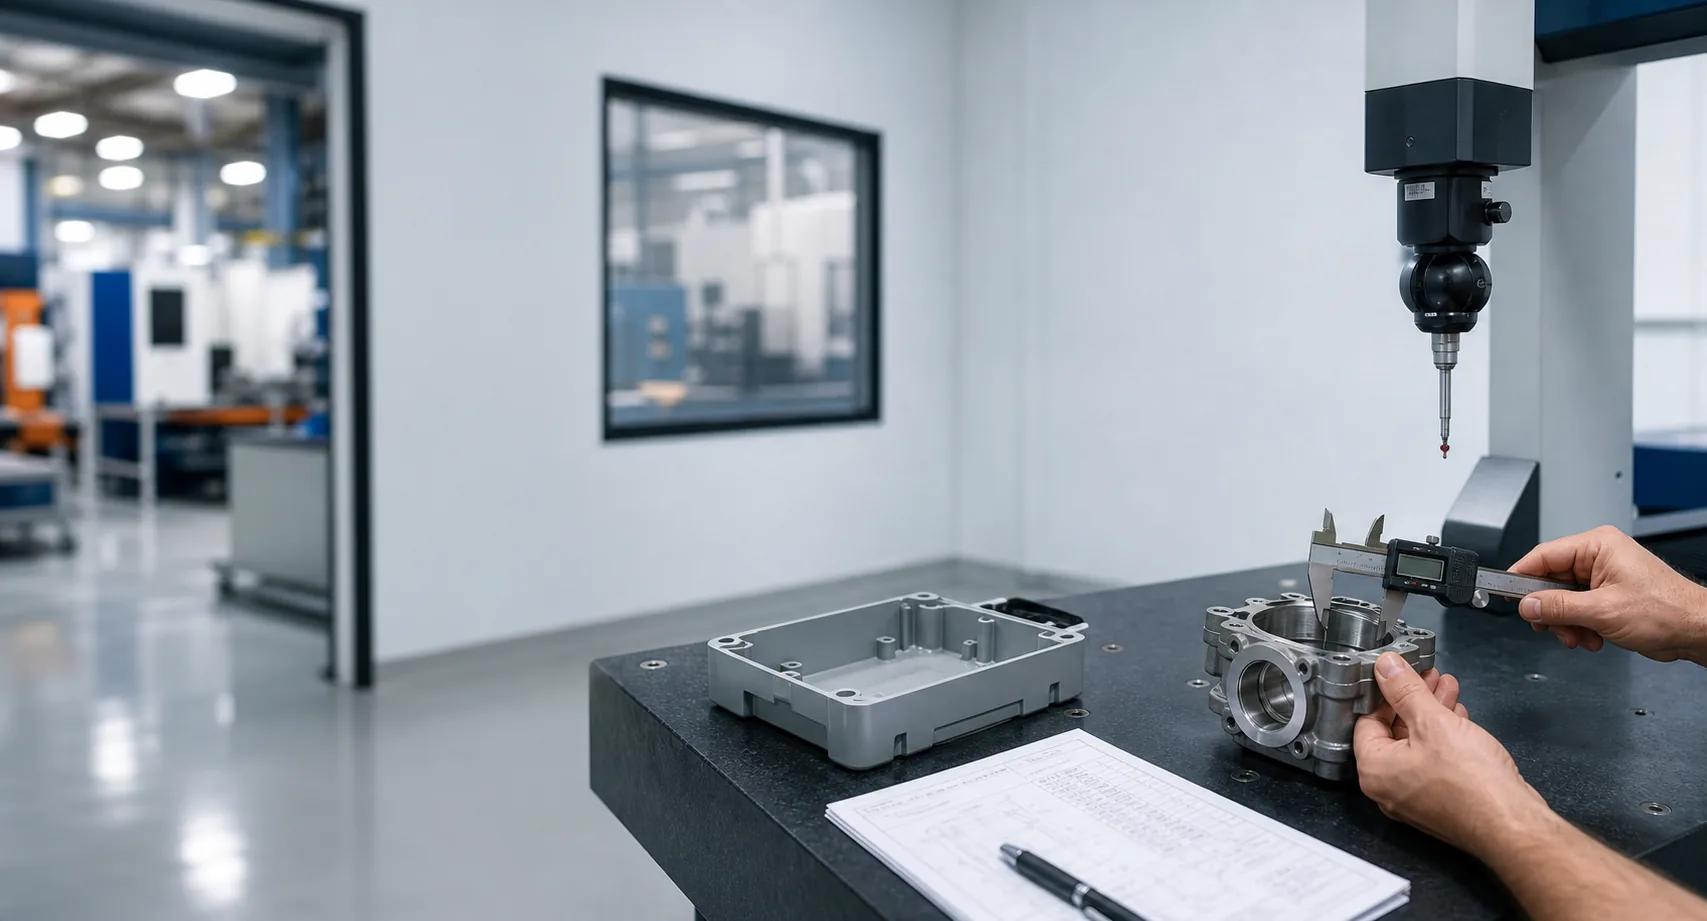
10 / Engineering Lessons
For energy-storage equipment, disciplined scope control is part of quality. A mechanical manufacturing partner should state exactly what it assembles and verifies, and what remains with the product owner or certification body.
This conclusion should remain tied to the documented engineering route and should be revised when real project evidence changes the lesson.
11 / Buyer FAQ
Yes, when the approved BOM, supplier responsibility, incoming criteria, substitution rules and assembly checks are defined.
Mechanical dimensions, fit, access, appearance, torque and packing checks can be scoped. Electrical, thermal and regulatory testing require explicit agreement.
Use controlled CAD, drawings, BOM revisions, approved deviations and a documented effective date for each change.
Provide released or clearly marked preliminary files, components, expected quantity, assembly sequence, acceptance criteria and issue-closure ownership.
14 / Request a Project Review
Share CAD or drawings, a sample where available, product use, material and finish direction, target quantity, bought-out components, destination, timing and the technical or commercial decision you need to make.